Pickleball paddle quality control for OEM and bulk orders
Three gates sit on every order, and eleven checkpoints run inside them. We weigh every paddle at 225 g ± 5 g, and the balance payment waits until you have seen the inspection record.
What we check
Weight, balance, thickness, bonding, foam, surface, print and grip.
When we check
First article on day 3 to 5, mid-run on day 15 to 20, pre-shipment on day 28 to 30.
What you get
A photo report and the weight log for the batch, sent before the balance is due.
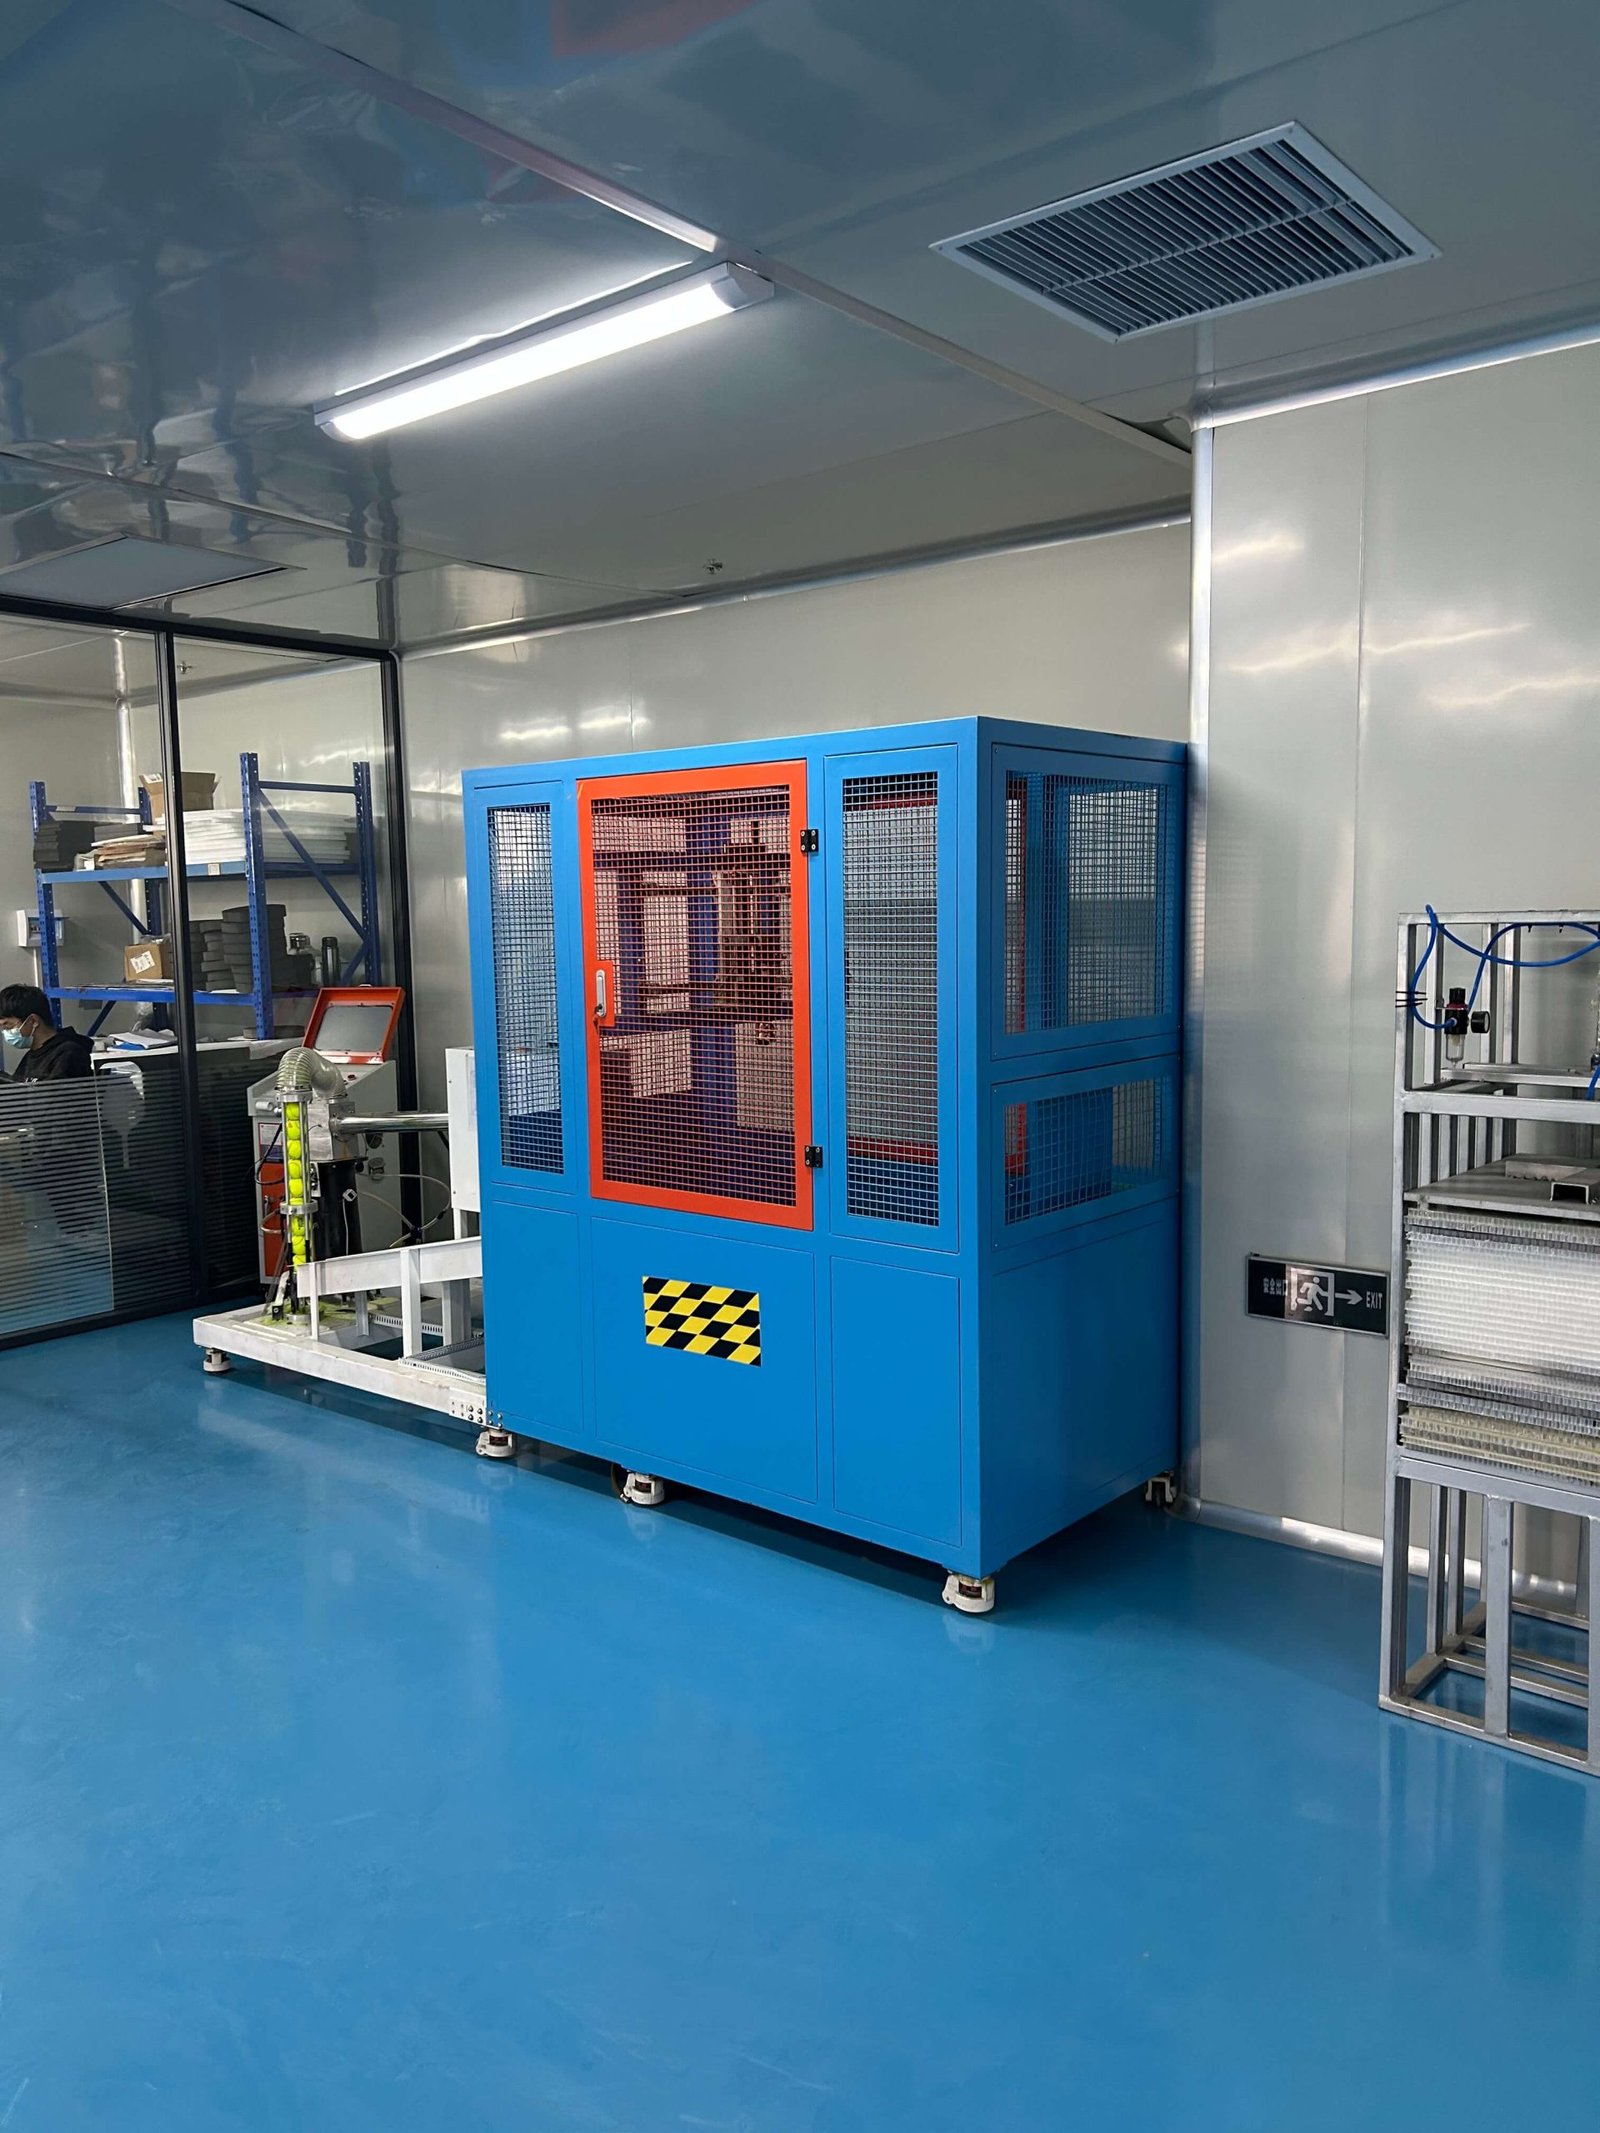
Four gates per order
A factory that only shows you final inspection photos is doing damage control, not control. The record has to start before the line starts, because most returns are decided by material that arrived two weeks earlier.
Gate 1 · before the line
Incoming material
We check the weave on the face sheet, the flatness of the honeycomb, the density of the foam, and the batch number on the glue film.
Gate 2 · day 3 to 5
First article
The first unit off the line gets photographed and measured, so you can stop a wrong mold before it runs 300 pieces.
Gate 3 · day 15 to 20
Mid-run
We re-weigh and re-map the thickness halfway through, because weight and thickness drift before appearance does.
Gate 4 · day 28 to 30
Pre-shipment
A random pick from each carton gets weighed, tapped, and photographed under a light box before the cartons close.
The days above assume a 2,000-piece order. A 200-piece order clears the same four gates inside about 30 days, and a 2,000-piece order takes about 35.
Six numbers behind feel
A buyer rarely complains that a paddle is badly made. The complaint is that the second carton does not feel like the first one, and each number below is one place that gap opens.
The eleven checkpoints
This list is the one buyers send us, word for word, in their first email. The right-hand column is what we hand over as proof, so you can audit the batch without standing in our factory.
| Checkpoint | How we measure it | How often | What you receive |
|---|---|---|---|
| Finished weight | Digital scale, target 225 g ± 5 g | Every unit | Batch weight log with the count per range |
| Balance | Balance jig, head and handle weighed separately | Sample, each batch | Balance reading per sampled unit |
| Surface roughness | Profilometer reading, Rz and Rt recorded | Sample, each batch | Reading plus a close-up of the same spot |
| Thickness | Five-point gauge map, 14 or 16 mm target | Each shift | Thickness map for the sampled units |
| Core bonding | Tap test along the edge, plus a cut section on one unit | Sample, each batch | Tap notes and the cut-section photo |
| Thermoforming | Temperature and pressure logged for every cycle | Every cycle | Cycle log for the run |
| Foam injection | Injected weight recorded, section checked for voids | Sample, each batch | Section photo at the edge |
| Edge guard | 3.2 mm overlap checked by hand and by eye on each color | Each colorway | Photo of the guard seam per color |
| Printing and graphics | Light box against the approved art file | Every unit | Daily sample photo from the line |
| Handle and grip | Circumference 101, 105 or 108 mm, plus a twist check | Sample, each batch | Circumference and twist notes |
| Final inspection | Random pick per carton, carton drop when the packaging changes | Every shipment | Inspection report before the balance is due |
The full checklist we work to sits in the pre-shipment inspection checklist that buyers can copy into their own purchase order.
Weight and balance
Weight is the one number a customer can check with a kitchen scale, so it is the number that starts a return. Balance is the number they cannot check, which is why we log it ourselves.
On a 216 g game paddle, 10 g more at the head adds about 2.0 kg·cm² of swing weight. The player feels that as a slower swing, not as a heavier paddle. Moving the balance point 8 mm toward the head shifts the balance by about 11.2%, and that is enough to turn a control paddle into a paddle that feels late.
We hold 225 g ± 5 g as the standard band because it covers the normal spread of a PP honeycomb core and a 16 mm build. When a brand sells matched pairs, we tighten the band to ± 2 to 3 g and weigh each pair against its partner instead of against the target.
Every unit is weighed before packing, and the log records how many fell into each 2 g bucket. That log is the first page you get, because it is the page that predicts your review score.
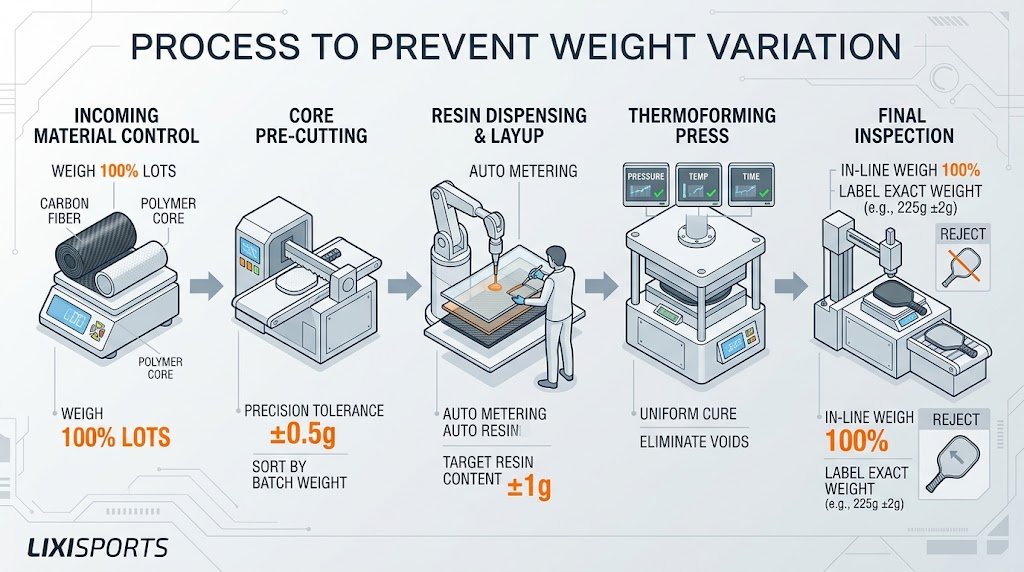
Weight spread across one production run. The scale catches a drift that the eye cannot see.
Thickness and dead spots
A paddle that measures 16 mm at the center can still be 15.4 mm near the upper corner, and the player who hits there calls it a dead spot. That is why we map five points instead of taking one number.
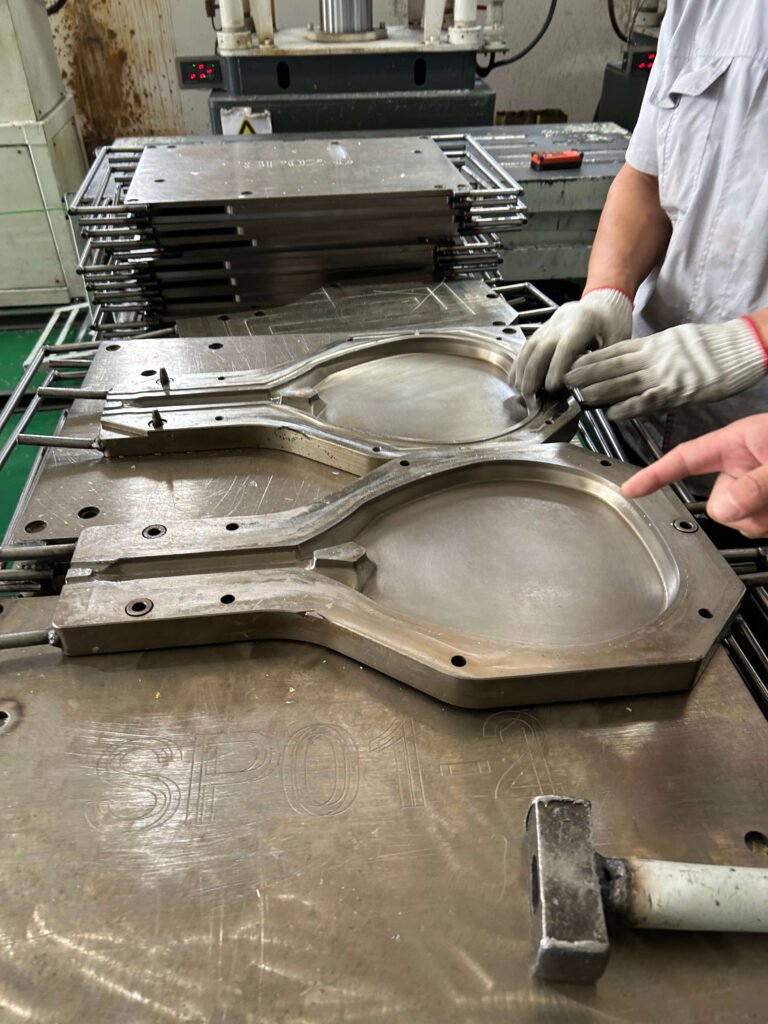
The mold fixes the outline and the thickness at the same time, so a thickness change is a mold change.
The thickness map runs at four corners and the center on every sampled unit, once per shift. A spread wider than 0.3 mm inside one paddle tells us the press is not sitting flat, and we stop and shim it before the next shift starts.
Core collapse is a separate problem, and it shows up later than thickness does. PP honeycomb cells crush under repeated hits, which is why a paddle that felt crisp in March can feel soft in September. EPP holds its shape better, but a density below 40 g/L takes a permanent set and never comes back.
Thickness is also a tooling cost, not a free setting. At our plant the 19 mm and 20 mm builds share one guard mold, and a jump from 16 mm to 20 mm needs a new mold and about 10 extra days.
Bonding and foam
Delamination, a collapsed core and a foam void look identical in a product photo. They come from three different places on the line, so they need three different checks.
The layers come apart
A tap along the edge sounds flat where the glue film did not bond. We sample every batch, and we keep the glue film batch number next to the press temperature for that run.
The core goes soft
PP honeycomb loses height after months of play. The fix is a different core, not a different glue, and we say so before the order rather than after the complaint.
The foam misses a corner
A void at the perimeter never shows on a finished paddle. We cut one unit per batch at the edge and photograph the section, because that is the only place a void is visible.
Cold press has one failure of its own. The neck can break where the handle meets the head, and molding a PU handle into that joint is what keeps our cold-press line shipping at the volume it does.
Surface and spin
A textured face loses grip as it wears, and the drop is what a brand feels in month four. Our own test fires 100 balls at 90 km/h at the same spot and reads the spin before and after.
On a ceramic sand infused face, spin fell from 1,668.83 to 1,621.99 RPM after 100 hits, which is a loss of 46.83 RPM. A conventional textured face loses roughly 100 RPM in the same test. That reading is taken on the unprinted face, because printing adds a layer the ball never touches in the same way.
We record roughness with a profilometer on every sampled batch and hand the reading over with a close-up of the same spot. We do not quote a roughness number we have not measured on that batch, because the same recipe can land in two different places when the resin cures differently.
The surface is also where graphics fail first. UV print on a glass fiber face can lift at the edge after a season of play, and raw carbon holds it better. If your program depends on a printed face, ask for the ceramic sand route instead of a sprayed coating.
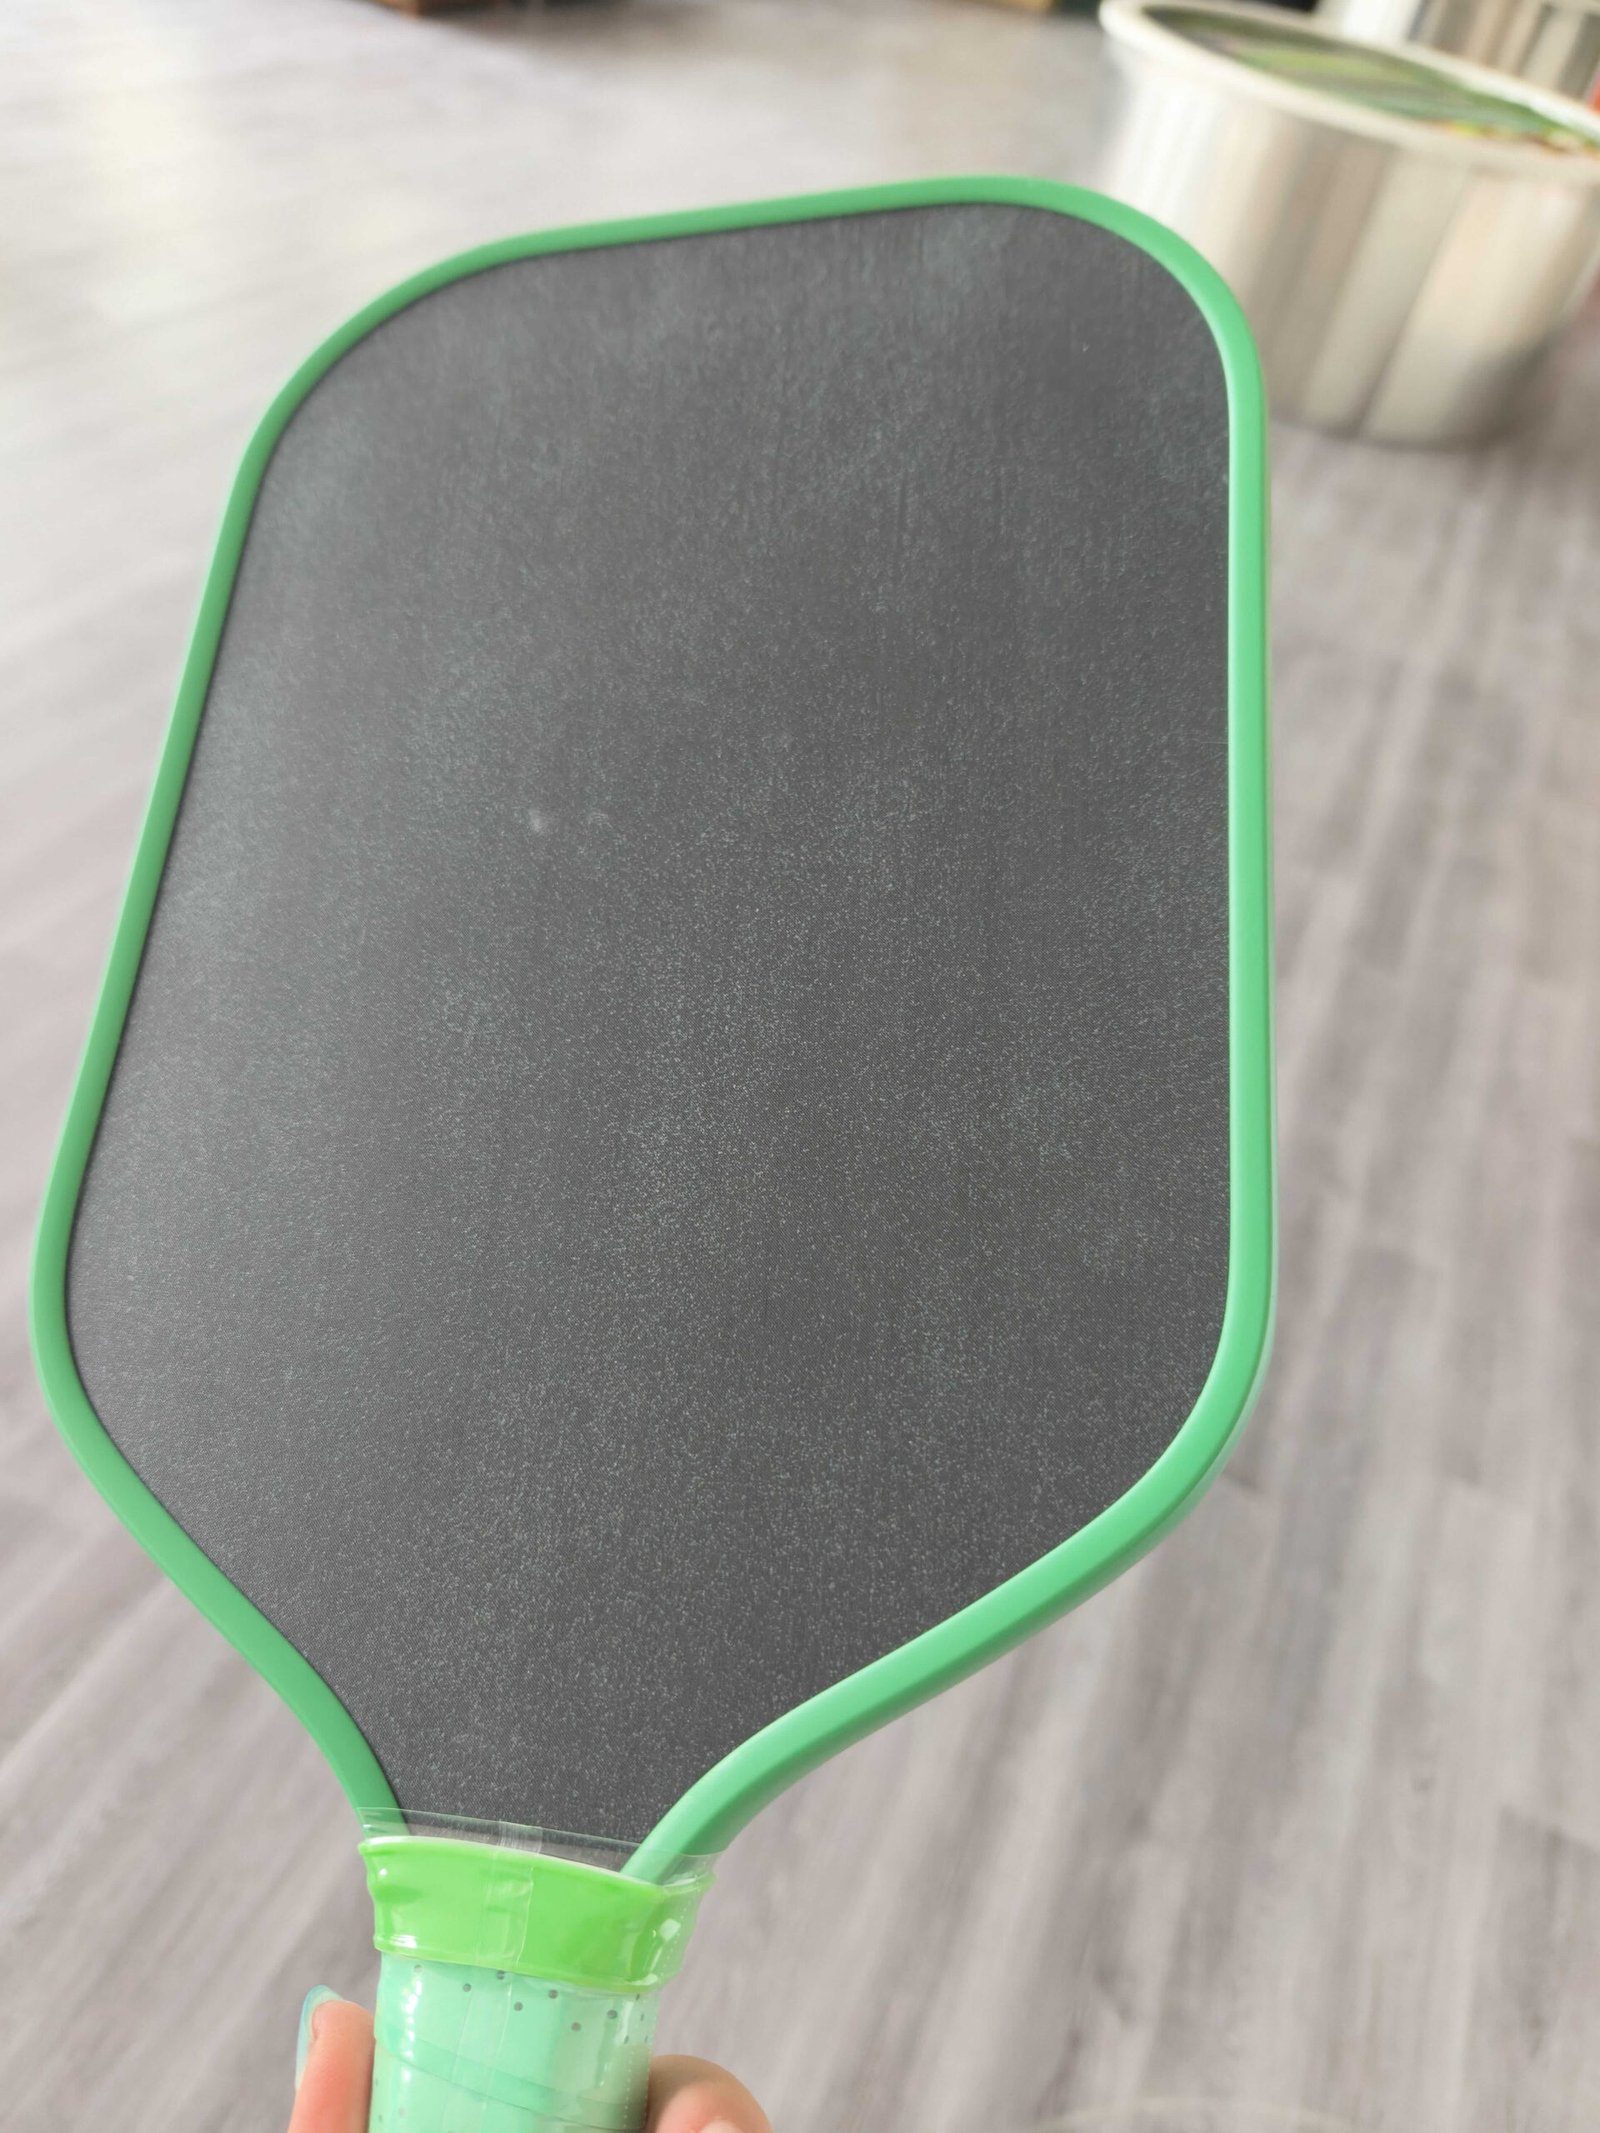
A face after wear testing. Grit cured into the resin stays put longer than a sprayed coating on the same sheet.
Print, grip and cosmetics
Nobody returns a paddle because the print sits 0.5 mm off center, but a shelf full of paddles with uneven print does not sell twice. Cosmetic checks run at 100% because they are cheap to do and expensive to miss.
Where the print lands
Every unit passes under a light box against the approved art file. The guard covers 3.2 mm of the face edge, so we keep 2 mm of clear ink inside that line and check the gap by eye.
Grip circumference
We hold three sizes at 101, 105 and 108 mm. A wrapped grip can vary by about 1 mm from unit to unit, and we tell you that instead of promising a number the wrap cannot hold.
Edge and end cap
The guard has to sit flush at the throat, where the two halves meet. A gap there collects dirt and reads as a factory second, so it is checked on each colorway.
What ships with the carton
You are buying a batch you cannot see, from a factory you may never visit. The pack below is the substitute for standing on the line, and it goes out before the balance payment is requested.
- Inspection report with photos of the sampled units, the print check and the carton markings.
- Weight log for the batch, counted in 2 g buckets against the 225 g target.
- Thickness map and roughness readings for the sampled units.
- Tap test notes and the cut-section photo from the foam check.
- Packing spec, plus a drop test result whenever the packaging changes.
- Written notice that a third-party inspector is welcome on the line at your cost.
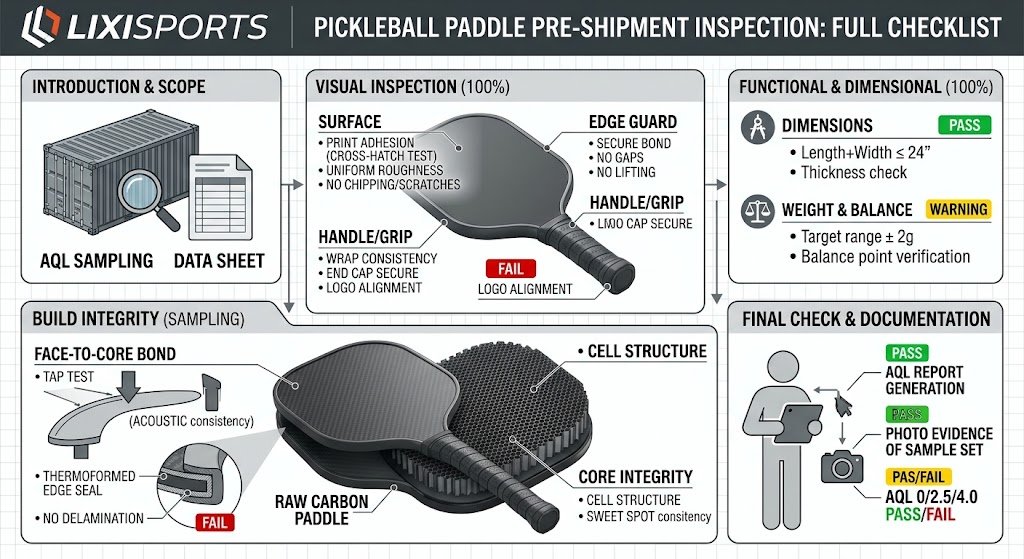
Pre-shipment inspection. Anything that fails here does not go into a carton.
The program these checks belong to, including the three build levels and the sample stage, is set out in our custom paddle program.
Where we stop
Every factory has a point where the checks run out. These are ours, and you should hear them before you pay a deposit rather than after a claim.
Five limits on this system
- Structure is checked on a sample, not on every unit. An X-ray scan or a cut section costs one paddle, so the units we inspect never go back into the carton.
- We will not publish a defect percentage before your specification is fixed. A rate quoted against an unknown spec is a guess, and a guess in a contract is worse than no number at all.
- A wrapped grip varies by about 1 mm from unit to unit. If your listing advertises an exact circumference, the wrap will not hold it to the decimal.
- We cannot certify your model. USA Pickleball approval is filed by the brand against a specific model, and we build to the published limits and run our own pre-check.
- Cold press will not give you a thermoformed feel, and no amount of inspection changes that. The construction sets the ceiling, and the checks only keep you near it.
Batches that fail a gate are held, not shipped. We find which gate missed the problem first, because a rework that skips that step ships the same defect twice.
Before you book an inspection
What is your standard weight tolerance?
We hold 225 g ± 5 g on every unit that ships. When a brand sells matched pairs, we tighten the band to ± 2 to 3 g and weigh each pair against its partner.
Do you weigh every paddle or only a sample?
Every unit goes on the scale before packing, and the count is logged in 2 g buckets. The other ten checks run on a sample plan, because they need a bench and an operator.
Can our own inspector visit the line?
Yes. Third-party inspectors such as SGS or Bureau Veritas are welcome during production and before shipment, and we book the slot once your deposit clears.
What happens when a batch fails a gate?
The batch is held and we look for the gate that missed the problem. We rework or replace the units before the cartons close, and we send you the photos of both the failure and the fix.
Do you test spin, or only measure roughness?
We fire 100 balls at 90 km/h at the same spot and read the spin before and after. A ceramic sand face lost 46.83 RPM in that test, against roughly 100 RPM on a conventional textured face.
How do you check the bond between core and face?
An operator taps along the edge on sampled units, and a flat sound marks a spot where the glue film did not bond. We also cut one unit per batch and photograph the section at the edge.
What defect rate do you accept?
We do not quote a percentage before your specification is fixed. What we put in writing is the checkpoint list, the pass rule for each one, and the report you receive with the batch.
Will mass production match the sample I approved?
We seal one golden sample at the factory and one on your side. The line compares against the sealed unit for feel as well as appearance, and that comparison is written into the run sheet.
Is the balance payment tied to the inspection?
Yes. Thirty percent starts production and the balance falls due after you approve the pre-shipment report. If the report shows a failure, the order stays on our floor.
Do you handle the USA Pickleball submission for us?
The brand files the submission, because approval attaches to the model and the brand name. We build the samples to the published limits and run a pre-check so a submission is not wasted.
Send the spec
Give us the face material, the core, the thickness and the target weight. We will come back with the pass rules for your build, the sample date, and the report you will receive before the balance.