Elongated pickleball paddle manufacturer and OEM factory
We cut the elongated footprint at 16.38 × 7.52 in with a 5.5 in grip and a 16 mm or 13 mm core. Cold-pressed or thermoformed, PP honeycomb, EPP or MPP inside, fiberglass to 18K carbon or ceramic sand on the face. MOQ is 200 pcs per design.
What it is
- A 16.38 × 7.52 in footprint, 23.90 in long plus wide against a 24.00 in ceiling.
- 0.38 in longer and 0.48 in narrower than our widebody.
- 5.5 in grip, 4.25 in handle, 225 g ±5 g target.
Where it wins
- Reach at the kitchen line without an extra step.
- A longer arc from the hand to the tip, so the tip travels faster at the same hand speed.
- A higher contact point on the serve and the overhead.
Where it costs you
- Swing weight rises even though the scale still reads 225 g.
- The face is narrow, so a miss toward the edge loses more ball speed.
- Lower twist resistance than the 8 in widebody.
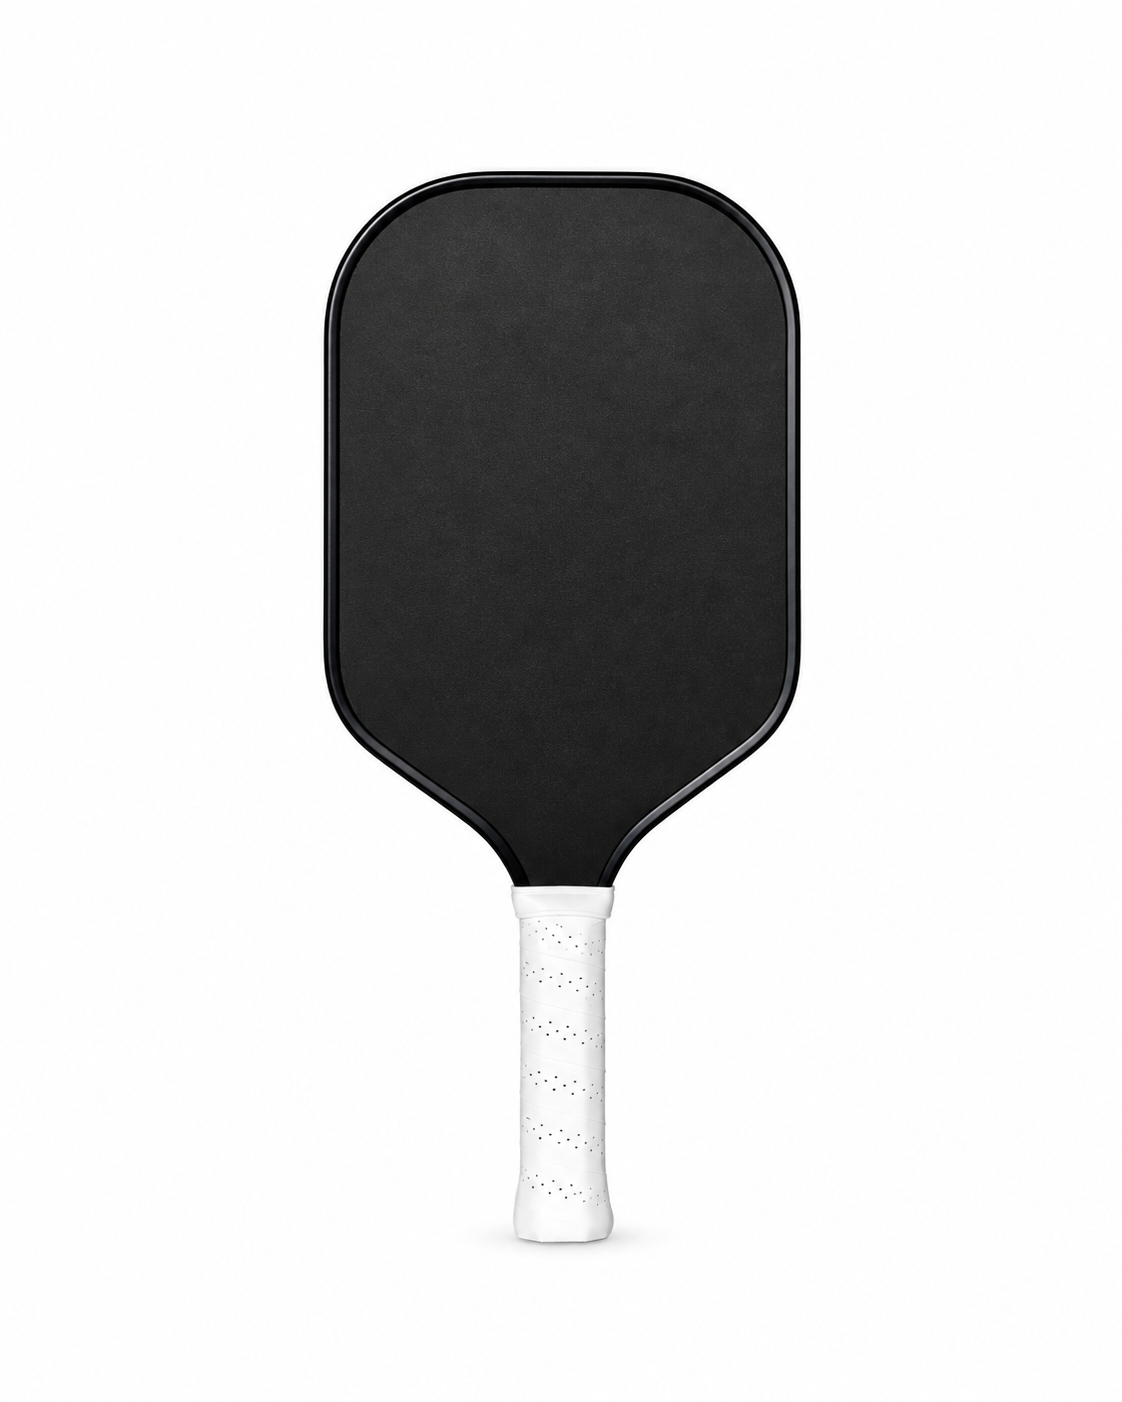
Extra length buys reach and charges you swing weight
Length is the one shape number that changes the distance from your hand to the ball. Everything else follows from that distance.
Our elongated face measures 16.38 in from the butt cap to the tip. The widebody measures 16.00 in. That 0.38 in, or roughly 9.7 mm, is the whole geometric difference between the two heads, and it changes three things at once.
Reach comes first. At the kitchen line a longer paddle covers more court without a step, and the serve and overhead are struck higher above the shoulder. Players who lose points to short reach notice this immediately.
Tip speed comes second, and the gain is small. Everything on the face swings on a longer radius, so the tip moves about 1% faster than the tip of a 16.00 in paddle at the same hand speed. That figure is arithmetic rather than a slogan, and it explains why a longer paddle feels like it hits harder than the geometry alone would suggest.
Swing weight comes third, and that is where you pay. Swing weight rises with the square of the distance from the hand, so moving the same 225 g outward along a longer frame makes the paddle heavier to swing. A paddle that reads 225 g on the scale can swing like a heavier paddle. If your buyers return paddles because they feel slow in a firefight, the elongated spec is the wrong place to look for an upgrade.
0.38 in more at the tip
Measured butt to tip against the 16.00 in widebody. At the kitchen line that is one less small adjustment step per dink exchange.
About 1% more tip speed
The tip travels a longer arc at the same hand speed. The gain is real and it is small, so sell the reach before you sell the power.
Higher swing weight at 225 g
The same mass sits further from the hand. Quick exchanges cost more energy even though the scale reads the same as your other SKUs.
A long, narrow sweet spot
The face is 7.52 in wide against 8.00 in on the widebody, so the forgiving band runs up the paddle rather than across it.
Swing weight belongs on the spec sheet next to static weight. Buyers compare your listing against a competitor that publishes both. When only one number appears, two paddles that read 225 g in both columns look identical until the first review lands.
The footprint we cut: 16.38 × 7.52 in, 23.90 in combined
These are cut dimensions taken off the mold rather than rounded marketing figures. Any change to one of them moves the order to a new mold.
| Item | Specification | Notes |
|---|---|---|
| Overall length | 16.38 in / 416 mm | Butt cap to tip. 17.00 in is the USAP ceiling. |
| Overall width | 7.52 in / 191 mm | Measured across the widest part of the head. |
| Length plus width | 23.90 in | 0.10 in under the 24.00 in USAP ceiling. |
| Grip length | 5.5 in / 140 mm | The wrapped surface. Custom lengths on request. |
| Handle length | 4.25 in / 108 mm | The shaft between the throat and the grip. |
| Grip circumference | 101 / 105 / 108 mm | Sizes 0, 1 and 2. PU wrap with printed logo. |
| Thickness | 16 mm standard, 13 mm on request | Same mold, so the footprint does not change with thickness. |
| Target weight | 225 g ±5 g | ±2 to 3 g on the Precision Program. |
| Process | Cold press or thermoformed | One-piece thermoform bonds the face, core and edge wall in a single cycle. |
| Core | PP honeycomb, EPP or MPP | All three fit the same mold without a footprint change. |
| Face | Fiberglass, T700 raw carbon, 3K / 12K / 18K carbon, Kevlar blend, ceramic sand infused | Sprayed grit on fiberglass. Raw weave left bare on carbon. |
| Edge | Edge guard or molded EVA perimeter | Colour matched to the graphics or the grip. |
| MOQ | 200 pcs per design | Tooling is quoted with the first order. |
| Sample lead time | 10 to 15 days | From an approved drawing. |
| Production lead time | 35 days | For orders up to 2,000 pcs after the sample is signed. |
| Capacity | 100,000 cold-pressed, 80,000 thermoformed per month | Two lines, Shenzhen and Vietnam. |
| Packing | PE bag and bubble bag | 50 pcs per 650 × 500 × 350 mm carton, about 12.5 kg. |
Length and width above are the overall footprint. The hitting face is smaller, because the throat narrows on both sides of the handle. The face dimensions on their own come from your drawing or from a physical paddle.
You have 0.10 in of headroom under the USAP combined rule
USA Pickleball runs two dimensional checks on a paddle. The combined figure is the one that catches long footprints.
Overall length has to be 17.00 in or less. Length plus width has to be 24.00 in or less. There is no separate width cap and no thickness cap inside the dimensional test, so the two numbers above are the whole story.
Our elongated footprint lands at 23.90 in. That leaves 0.10 in, or about 2.5 mm, between the cut and the ceiling. The margin sounds comfortable until you look at how the finished part is measured. A paddle is gauged with the edge guard fitted, and the guard adds a small amount to the width. A mold that runs 1 mm long eats 40% of that budget before the guard goes on.
We hold the mold under the published figure and gauge finished parts against the same two numbers the test lab uses. All three of our shapes are cut close to the ceiling on purpose. Only one of them has no room left at all.
| Shape | Length | Width | Length + width | Headroom under 24.00 in |
|---|---|---|---|---|
| Elongated | 16.38 in | 7.52 in | 23.90 in | 0.10 in / about 2.5 mm |
| Hybrid | 16.30 in | 7.68 in | 23.98 in | 0.02 in / about 0.5 mm |
| Widebody | 16.00 in | 8.00 in | 24.00 in | 0.00 in |
Figures are our cut dimensions before the edge guard. Confirm the total with the guard fitted if your lab measures the finished paddle.
Approval is a brand filing, per model. We build to the published dimensional and surface targets, and we hand you the measurements with each batch. No factory can certify your SKU on your behalf, and any supplier who says otherwise is describing something that does not exist.
Where the limits come from: equipment.usapickleball.org publishes the paddle test standard and the approved list. Our own walkthrough of both certifying bodies is in the USAP certification guide.
The core decides whether that extra length feels controlled
A longer face puts more material ahead of the hand. The material inside that face decides how the paddle behaves on an off-centre hit.
All three of our cores come off the same 16.38 × 7.52 in mold. Swapping between them changes the price, the rebound and how the paddle holds up over a season, and it does not change the footprint your listing publishes.
Core choice leaves the spin number where it was. Spin comes from the face material and its texture, so a spin test reads the same for a honeycomb core and an EPP core sitting behind the same face. Buyers who ask for the core that spins more are asking about the wrong component.
PP honeycomb
The default core in the market and the stiffest of the three. Cell size runs 8 or 10 mm, wall thickness 30 to 90 µm, density 60 to 90 g/L. It returns energy fastest, which is what makes a long face feel powerful.
It is also the core that goes flat. Repeated hits crush cells, and a face that has lost its rebound reads as dead without showing any visible damage.
EPP foam
Closed-cell beads with a density range of 20 to 200 g/L. We run 60 g/L for a light build, 80 g/L as the standard, and 100 g/L when the buyer wants the paddle to feel planted.
It recovers its thickness after a hard hit, so a long face keeps its shape through a season. It also damps more than honeycomb, so the tip feels softer rather than faster.
MPP microcellular
Microcellular polypropylene with cells under 100 µm, run at 45 to 90 g/L with 60 g/L as the starting grade. The continuous cell wall carries stiffness and toughness in the same part, which is why it does not collapse under a hard hit.
It is the most expensive of the three, because the foaming window is about 15 °C wide and the material has to be a high-melt-strength grade.
| Core | Density we run | What it does on a 16.38 in face | Cost position |
|---|---|---|---|
| PP honeycomb | 60 to 90 g/L | Fastest rebound. Goes flat over a season of hard play. | Lowest |
| EPP | 60 / 80 / 100 g/L | Keeps its thickness and damps the tip. Softer response. | Middle |
| MPP | 45 to 90 g/L, 60 start | Stiff and tough at once. Longest cell life under repeated impact. | Highest |
The longer versions sit in PP honeycomb cores, EPP cores and every core and face we run.
The face sets how the tip feels and how long the grip lasts
A longer face amplifies whatever the outer ply does, because the tip is the part that moves fastest through the contact.
| Face | Surface | What it gives you on a long face | Where it fits |
|---|---|---|---|
| Fiberglass | Sprayed grit over the resin | Softest response and the most forgiving contact. Lowest cost of the group. | Entry and mid builds, club orders |
| T700 raw carbon | Woven, left bare | Firm contact and a weave that keeps its texture instead of polishing smooth. | The volume seller |
| 3K / 12K / 18K carbon | Woven, ply count changes | Wider weave reads softer and less uniform. 18K is the softest of the three tow counts. | Premium builds |
| Kevlar blend | Aramid and carbon together | Tough and damped. It does not add pop, so pair it with a control brief rather than a power one. | Premium control builds |
| Ceramic sand infused | Ceramic particles cured in the resin | Holds grip after a plain weave would have polished smooth. Highest face cost. | Premium, long-grip-life briefs |
Our own bench numbers on the ceramic face. We fire a ball at 90 km/h into a paddle face 100 times and read the spin before and after. One of our ceramic sand faces dropped 46.83 RPM across the run. A conventional textured face on the same rig dropped about 100 RPM. That is a 2.1 times difference in grip retention.
Those numbers come from our bench, on our samples, and they describe one face against one face. They come off a factory rig rather than a laboratory, and they say nothing about your model. The measurement matters here for one reason. A longer face exposes more surface area to the ball, so wear spreads across a bigger area. A player feels the gap between a face that holds grip and one that has gone smooth.
The full build and the test method sit in how the ceramic grit face is built.
Cold press or thermoform, and where each one lands
Both processes cut the same elongated shape. They differ in heat, in pressure, and in what you are allowed to put on the face.
Cold press
The face and core cure at room temperature. Fiberglass and carbon faces run here, with PP honeycomb behind them in most orders.
The shape comes from a trimmed dieline rather than a mold, so a fiberglass elongated paddle does not need shape tooling. That is the fastest and cheapest route to a first elongated SKU, and it is why most brands start here.
Thermoformed
Heat and pressure cure the face, the core and the edge wall in one cycle. The result is a stiffer, more consistent paddle with an edge that cannot peel away from the core.
Kevlar needs this route. A cold-pressed aramid rim frays during trimming, and the fray shows up as fuzz along the edge. Ceramic sand and molded EVA perimeters also run here.
| Cold press | Thermoformed | |
|---|---|---|
| Cure | Room temperature | Heat and pressure in one cycle |
| Face options | Fiberglass, carbon, sprayed grit | Every face, including Kevlar and ceramic sand |
| Edge | Separate edge guard fitted after trimming | Molded edge wall, or an EVA perimeter with no separate guard |
| Shape tooling | Cut pattern for fiberglass, no shaped mold | Tooling mold per footprint |
| Where it sits in the market | Entry, mid and club lines | Mid to premium lines |
| Monthly capacity | 100,000 pcs | 80,000 pcs |
The sample window and the tooling step both move the total lead time, and what sets the lead time breaks that down.
What you can change before the mold is cut
Every item below is quotable in the same program. The one thing that resets the clock is the footprint, because that is the part made of steel.
Footprint
16.38 × 7.52 in is our recommended elongated cut. A different length or width means a new mold, and a shape approved after tooling starts cannot be edited back.
Grip and handle
5.5 in grip and 4.25 in handle as standard, with 101, 105 or 108 mm circumference. Grip wrap colour and printed logo are quoted with the order.
Edge and graphics
Edge guard colour to match the graphics, or a molded EVA perimeter on a thermoform build. UV print on fiberglass, bare weave on carbon, dyed ceramic on the sand face.
Weight and balance
225 g ±5 g as standard, or ±2 to 3 g on the Precision Program. Balance is set at sample stage by moving mass between the head and the handle.
End cap and band
Custom end cap and silicone band, in the same colour program as the grip and the edge.
Packaging
PE bag and bubble bag by default, 50 pcs per carton. Retail boxes, hangtags and master carton print are quoted separately.
Grip length and handle length are two different measurements. Grip length is the wrapped surface a hand covers. Handle length is the shaft between the throat and the butt cap. Your product listing publishes one of the two, and we cut the drawing to that number rather than guessing from the other.
A new footprint, a new core and new graphics each move the MOQ and the sample window. The mechanics are in what a custom shape order covers and in the sample sign-off list.
Which buyers should order elongated, and which should not
Order elongated if your line needs a power model with real reach. Do not order it if your buyers are beginners or your SKU list has room for only one shape. A shape is the one decision that cannot be adjusted after tooling, so match it to the player before the sample stage.
| Your buying situation | What the elongated face gives you | Our advice |
|---|---|---|
| You want a power model above an all-court SKU | A longer arc, real reach at the kitchen line and a higher serve contact point | Order it. |
| Your buyers are rated 3.5 and below | Reach matters less than forgiveness, and the narrow face punishes off-centre contact | No. Take the widebody. |
| Your players live at the kitchen line in long dinks | The reach saves a step, but the higher swing weight costs you in a firefight | Order it only if the model is sold as power. |
| Your listing quotes static weight and nothing else | 225 g on the scale, heavier in the hand than the widebody | Add swing weight before launch. |
| You need one SKU to cover the whole market | Elongated excludes the beginner end of the range | No. Start with the hybrid. |
| You sell to an advanced club or a tournament player | Reach, a high contact point, and a face that stays flat longer when you order EPP or MPP | Order it in the premium build. |
Alternatives we quote the most: the hybrid at 16.30 × 7.68 in when a buyer wants a single SKU. The widebody at 16.00 × 8.00 in is the other one, for when forgiveness beats reach. Buyers ordering for clubs and schools usually land on the widebody as well. The reason sits in club and school programs. All three sit under the same 24.00 in rule, and the three footprints drawn to one scale show how little separates them.
Where the elongated shape is the wrong answer
Five things we will not claim
- A longer face raises swing weight at the same static weight, and no core choice removes that. Balancing the handle lightens the head, but the mass still sits further out along a longer frame.
- The narrow face is a real limit for beginners. Players rated below 3.0 lose more on side mishits than they gain in reach, and the reviews will say the paddle is unforgiving.
- We publish no swing weight figure here. Swing weight depends on your core, your face and your balance point, and it is measured on a finished paddle rather than read off a drawing.
- A shape change after tooling starts is a new mold. If you approve a 16.38 in sample and later ask for 16.00 in, the first mold is scrap and the lead time restarts.
- The 0.10 in of headroom is thinner than it sounds. Any footprint we cut for you sits close to the 24.00 in ceiling, so a supplier who promises a longer paddle and a wider face at the same time is describing something the rule does not allow.
The records that come with the order
Everything below is a measurement we take on your order. None of it is a certification, and none of it replaces the approval your brand files.
X-ray on every new build
We image the layup before the run starts, so a dry ply or an air gap shows up on the film instead of in a customer's hand.
Ball cannon, 90 km/h, 100 hits
Spin is read before and after the run. It is the closest thing we have to a season of play in one afternoon.
Compression test on bulk samples
Samples are pulled from the production run rather than from the sample table, so the number describes what you will actually receive.
In-house USAP and PBCoR pre-check
We measure against the published targets before shipping, so a surprise at the lab is less likely. The filing itself stays with your brand.
QC report per batch
Dimension, weight, thickness and balance for every batch, recorded against the signed sample rather than against a nominal figure.
Pre-shipment check
A twelve-point inspection on the packed cartons before they leave the factory. The full list is in the pre-shipment checklist.
The factory runs a BSCI social audit and an ISO 9001 quality system. We describe how a sample is measured against these records in how we test a sample.
Elongated paddle questions buyers ask before tooling
Is an elongated paddle legal for USAP play?
Yes. USA Pickleball checks overall length at 17.00 in or less and length plus width at 24.00 in or less. Our elongated footprint is 16.38 in by 7.52 in, which adds up to 23.90 in.
What is the MOQ for a custom elongated paddle?
200 pcs per design. A new footprint needs its own mold, cut for the fiberglass line or for a thermoformed build, and that tooling is quoted with the order.
How long does an elongated sample take?
10 to 15 days from an approved drawing. Production for up to 2,000 pcs runs about 35 days after the sample is signed off.
Can I order the elongated shape in 13 mm instead of 16 mm?
Yes. The footprint does not change with thickness, so 13 mm and 16 mm come off the same shape. We keep 16 mm as the default because most buyers ask for it, and 13 mm is quoted from the same tooling.
Does an elongated paddle spin more than a widebody?
No. Spin comes from the face material and its texture. Two paddles with the same face read the same on a spin test no matter how long the footprint is.
Which core suits a longer face?
PP honeycomb returns energy fastest and costs the least. EPP holds its thickness longer and damps more. MPP gives stiffness and toughness in one part and costs the most. All three fit the same mold, so the choice is about the brief rather than the tooling.
Can you match another factory's elongated footprint?
The drawing or a physical paddle is enough, and we measure it here. We will also give you the length-plus-width total, because a footprint that measures 24.05 in will fail the USAP dimensional check even if it feels fine in the hand.
Does the paddle ship USAP certified?
No. Approval is filed by the brand, per model. We build to the published dimensional and surface targets and give you the measurements with each batch.
How is the order packed?
PE bag and bubble bag as standard, 50 paddles per 650 by 500 by 350 mm carton at about 12.5 kg. Custom retail packaging is quoted separately.
Can you make the grip longer for a two-handed backhand?
Yes. Grip length and handle length are separate dimensions, and lengthening the grip moves the balance point toward the hand. Confirm both numbers on the drawing before the mold is cut, because the handle is molded with the head on a thermoform build.
Send the footprint. Get a sample plan and a quote.
With the length, the width, the core and the face in hand, we confirm the combined figure against the 24.00 in rule before anything is cut. A photo of a competitor paddle is enough to start, and we measure the drawing from it.
Email goes to lixifirm@outlook.com, and we answer within 24 hours.